
关键词:
咨询电话:
熊经理 18168863192
周经理 13665101927
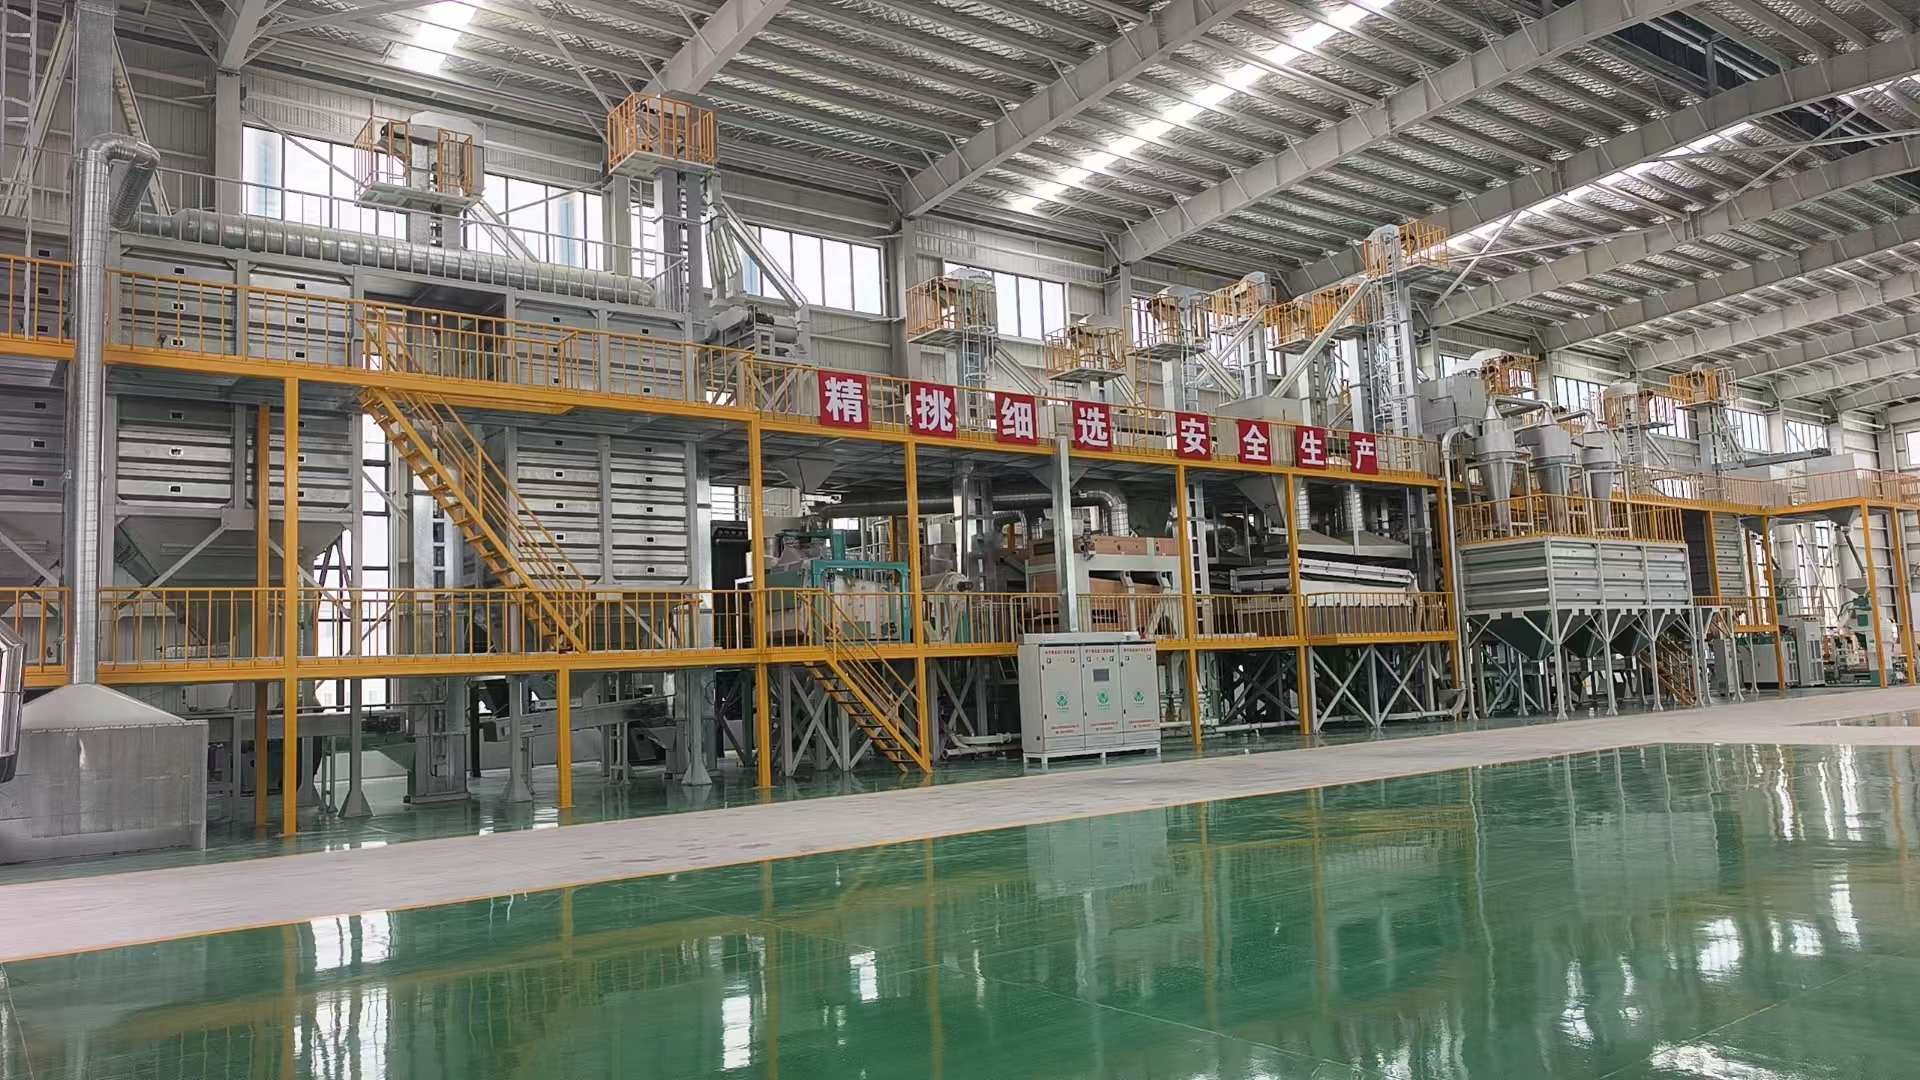
5CTSD-15A种子清选、包装、码垛成套设备
设计思路与方案
本成套设备针对谷物种子清选、分级、包衣、定量包装、自动码垛等全流程加工需求,集物料提升输送、种子除芒、初清、风选、筛选、比重分选、谷糙分离、光电色选、定量包装、机器人码垛、脉冲除尘、杂质自动收集及全自动电气控制系统于一体,可实现种子从原料投入至成品码垛入库的全流程连续化、自动化、智能化作业。
设备可高效剔除原料中掺杂的秸秆、尘土、石子、瘪粒、破碎粒、霉变病变粒、异种杂粒等各类杂质,完成种子精准除杂,有效精选出活力强、发芽率高、品相优良的优质种子,大幅提升成品种子净度与整体品质,保障种子播种后的出苗质量与种植稳定性。
一、人性化节能设计,降本增效、省工提质
设备以用户实际生产需求为核心设计,秉持省力化、低能耗、高效率的设计理念,大幅降低人工与运维成本。整套生产线仅原料上料环节需1名操作人员值守,后续清选、分选、包装、码垛、杂质收集、除尘净化等所有工序均实现全自动无人化作业。各单机设备之间无缝对接、自动联动运行,无需人工干预值守,极大缩减人工投入,有效降低企业用工成本与管理成本。
在节能降耗层面,设备所有额定功率4kW以上的电机均配置变频器软启动控制系统,彻底解决传统电机启动电流大、瞬时能耗高、设备冲击大的问题。同时支持电机变频调速运行,可根据不同水稻品种、加工工况灵活调节运行转速,无需设备满负荷运转即可达到最优加工效果,精准匹配生产需求,持续实现节能降本、提质增效的生产目标。
二、智能自动化控制系统,灵活可控、安全稳定
整套设备采用PLC可编程控制器集中控制,搭载双模式操作系统,支持15英寸高清触摸屏智能操控与传统物理按钮操控自由切换,适配不同操作人员的使用习惯。全线设备搭载高精度运行监测传感器与智能料位检测模块,可实时采集、反馈各设备运行状态、物料输送工况,运行数据可视化呈现。当设备出现异常工况时,系统将自动触发紧急停机机制,同步启动声光报警提示,并在触摸屏界面精准定位故障点位、显示故障成因及标准化排查与解决方案,大幅降低设备故障排查与维修难度,保障生产连续稳定运行。
设备操作界面搭载动态仿真工艺流程画面,直观呈现全线生产状态。系统支持工艺流程柔性可调,可根据不同水稻种子加工工艺需求、生产规模灵活调整作业流程。设备支持整机联动运行、多机组合运行、单机独立启停三种作业模式,无需全线空载试运行,适配多样化生产场景,操作灵活便捷。同时内置防误操作程序,针对违规操作、误操作指令自动拒绝执行,从程序层面规避人为操作失误带来的设备故障与生产风险,设备运行安全性与容错性大幅提升。
三、无损伤提升设计,杜绝籽粒破碎、降低加工损耗
针对长粒型或大颗粒种子易折断、易碾碎、易破壳的物料特性,本设备全线采用Z型无破碎专用提升机,摒弃传统斗式提升机对籽粒碾压的结构弊端,彻底解决物料提升过程中对籽粒挤压、折断、破碎等问题。全程实现种子柔性输送、无损提升,确保经过清选后的优质种子零损伤、零增碎,有效降低原料加工损耗,提升成品种子产出率,最大化提升用户生产经济效益。
四、模块化除尘系统设计,洁净高效、运维便捷
为保障种子清选加工车间生产环境洁净、规避粉尘污染,本方案配套专属除尘布局设计。在设备安装侧的室外区域,设计了规格3米宽×3米高的平顶集灰房,房顶承重标准≥2吨/㎡。将脉冲除尘器及除尘风机一体化布置于集灰房屋顶,屋面落灰位置精准开孔并设置防水反坎结构,实现除尘杂质、粉尘统一收集至集灰房内部。该设计可实现粉尘、杂质集中归集,在种子加工生产周期内无需人工频繁清灰,仅需淡季空闲时集中清理即可,大幅减少人工运维工作量。同时集灰房全域配置防爆灯具、防爆开关,严格杜绝明火隐患,保障车间生产安全,从源头优化种子加工生产环境。
五、标准化集中供气系统,供气稳定、适配性强
设备配套了集中供气系统,采用变频螺杆空压机为核心制气设备,搭配2台1m³储气罐稳定储气,配置冷冻式冷干机去除压缩空气中的水分、水汽,再通过三次纳米级高精度过滤器完成空气净化过滤,彻底去除压缩空气中的水分、杂质、油污。净化后的高压气体通过耐腐蚀非金属管网统一布线输送至各用气单机设备,全程供气稳定、洁净、无杂质,可有效保障气动部件精准、稳定运行,延长设备气动组件使用寿命。
六、耐磨式溜粮管道设计,免维护、降耗材
针对谷物输送管道易磨损、易损耗、需频繁更换的行业痛点,本设备的谷物输送管道全部采用高耐磨玻璃材质,具备耐腐蚀、抗冲刷、零磨损的特性,可彻底解决传统金属管道易磨损、磨破等问题。大幅降低设备日常运维频次,减少易损件更换成本,降低设备后期运维投入,提升设备长期运行的稳定性与可靠性。
七、密闭式气力集杂系统,高效集杂、杜绝泄压
种子清选加工成套设备采用全密闭气力负压集杂技术,各单机设备筛选剔除的杂质,通过管道高负压吸力实现无损抽吸,统一归集至专用集杂仓。所有设备排杂口与抽吸管道对接位置均配置密闭式旋转阀,依托旋转阀“只进物料、不漏气压”的工作原理,彻底杜绝管道漏气、泄压、吸杂无力等问题,保障集杂系统持续高效稳定运行,确保杂质彻底、干净收集杂质。
八、核心技术参数与性能指标
本设备各项性能指标严格遵循GB/T 21158-2025《种子加工成套设备》国家标准,核心参数如下:
1. 加工生产率:以小麦为基准5-15t/h;
2. 种子净度:≥99%;
3. 种子获选率:≥99%;
4. 光电选净率:≥99%;
5. 包装成品合格率:≥99.9%;
6. 破碎率增值:≤0.01%;
7. 车间粉尘浓度:≤8mg/m³;
8. 设备运行噪声:≤85Db(A)。
注:以上指标基于种子原始净度符合国标标准前提下测得。
This complete set of equipment is developed for the full-process processing requirements of grain seeds, including seed cleaning, grading, coating, quantitative packaging and automatic palletizing. It integrates material lifting & conveying, seed de-awning, pre-cleaning, air separation, screening, specific gravity separation, husked rice separation, photoelectric color sorting, quantitative packaging, robotic palletizing, pulse dust removal, automatic impurity collection and fully automatic electrical control system. It enables continuous, automatic and intelligent full-process operation of seeds from raw material feeding to finished product palletizing and warehousing.
The equipment can efficiently remove various impurities mixed in raw materials, such as straw, dust, stones, shrunken grains, broken grains, mildewed & diseased grains and foreign grains. It completes precise impurity removal of seeds, and effectively selects high-quality seeds with strong vitality, high germination rate and good appearance. It greatly improves the purity and overall quality of finished seeds, and guarantees seedling emergence quality and planting stability after sowing.
Centered on users’ actual production demands, the equipment adopts the design philosophy of labor saving, low energy consumption and high efficiency, so as to greatly reduce labor and operation & maintenance costs. For the whole production line, only one operator needs to be on duty at the raw material feeding station. Subsequent procedures including cleaning, sorting, packaging, palletizing, impurity collection and dust purification all realize fully automatic unattended operation. Each single machine is seamlessly connected and operates in automatic linkage without manual intervention, which drastically cuts labor input and lowers corporate labor and management costs.
In terms of energy conservation and consumption reduction, all motors with rated power above 4 kW are equipped with frequency converter soft-start control systems, which thoroughly solve the problems of large starting current, high instantaneous energy consumption and heavy equipment impact of traditional motors. Meanwhile, the motors support variable-frequency speed regulation. The rotating speed can be flexibly adjusted according to different rice varieties and processing working conditions. Optimal processing results can be achieved without full-load operation, precisely matching production requirements and continuously realizing the production goal of energy saving, cost reduction, quality improvement and efficiency enhancement.
The complete set adopts a PLC programmable logic controller for centralized control, equipped with a dual-mode operating system. It supports free switching between intelligent operation via a 15-inch high-definition touch screen and traditional physical button operation, adapting to the operating habits of different operators. High-precision operation monitoring sensors and intelligent material level detection modules are deployed along the whole line to collect and feedback real-time operating status of each equipment and material conveying conditions, with visualized presentation of operating data.
In case of abnormal working conditions, the system will automatically trigger emergency shutdown, activate audible and visual alarms synchronously, accurately locate fault points on the touch screen, display fault causes as well as standardized troubleshooting and solutions. It greatly reduces the difficulty of fault diagnosis and maintenance, and ensures continuous and stable production.
The operation interface is equipped with a dynamic simulation process flow chart to intuitively display the whole-line production status. The process flow supports flexible adjustment, which can be modified according to different rice seed processing requirements and production scales. Three operation modes are available: whole-line linkage operation, multi-machine combined operation and independent start-stop of single machine. No no-load trial run of the whole line is required to adapt to diversified production scenarios with flexible and convenient operation. Meanwhile, an anti-misoperation program is built in, which automatically rejects illegal and misoperation instructions. It avoids equipment failures and production risks caused by human misoperation from the program level, and greatly improves operation safety and fault tolerance of the equipment.
Aiming at the material characteristics of long-grain or large-particle seeds which are prone to breakage, crushing and shell cracking, the whole line is equipped with Z-type special non-breakage elevators, abandoning the structural drawback of grain rolling in traditional bucket elevators. It completely eliminates extrusion, snapping and breakage of grains during material lifting, realizing flexible conveying and non-damaging lifting of seeds in the whole process. It ensures zero damage and zero additional breakage of high-quality seeds after cleaning, effectively reduces raw material processing loss, improves the yield of finished seeds, and maximizes users’ production economic benefits.
To guarantee a clean production environment in the seed cleaning workshop and avoid dust pollution, this scheme is equipped with a dedicated dust removal layout. A flat-topped ash collecting house with dimensions of 3 m × 3 m is built outdoors beside the equipment installation area, with roof bearing capacity ≥ 2 t/㎡. Pulse dust collectors and dust removal fans are integrally arranged on the roof of the ash collecting house. Holes are precisely opened at ash falling positions on the roof with waterproof reverse sills, so that dust and impurities from dust removal can be uniformly collected into the ash collecting house.
This design realizes centralized collection of dust and impurities. Frequent manual ash cleaning is unnecessary during the seed production cycle; centralized cleaning is only required in off-seasons, which greatly reduces manual operation & maintenance workload. Meanwhile, explosion-proof lamps and explosion-proof switches are installed throughout the ash collecting house to thoroughly eliminate open fire hazards, ensure workshop production safety, and optimize the seed processing environment from the source.
The equipment is matched with a centralized air supply system, adopting a variable-frequency screw air compressor as the core gas generation equipment, together with 2 sets of 1 m³ air storage tanks for gas stabilization. A refrigerated air dryer is configured to remove moisture and water vapor in compressed air, followed by three-stage nano high-precision filters for air purification, which completely removes moisture, impurities and oil stains in compressed air.
The purified high-pressure gas is delivered to each single air-consuming equipment through corrosion-resistant non-metallic pipe networks with unified routing, featuring stable, clean and impurity-free air supply in the whole process. It can effectively guarantee accurate and stable operation of pneumatic components and extend the service life of pneumatic assemblies.
In response to the industry pain points of easy wear, high loss and frequent replacement of grain conveying pipelines, all grain conveying pipelines of this equipment are made of high-wear-resistant glass material, featuring corrosion resistance, erosion resistance and zero wear. It completely solves the problem of easy wear and rupture of traditional metal pipelines. It greatly reduces the frequency of daily equipment maintenance, lowers the replacement cost of wearing parts, cuts the later operation & maintenance investment of the equipment, and improves the stability and reliability of long-term operation.
The complete seed cleaning equipment adopts fully closed negative-pressure pneumatic impurity collection technology. Impurities screened and discharged by each single machine are extracted by high negative pressure in pipelines and uniformly collected into a special impurity bin. Closed rotary valves are installed at the joints between impurity discharge ports and suction pipelines. Based on the working principle of rotary valves that "materials can pass through while air pressure cannot leak", pipeline air leakage, pressure drop and insufficient impurity suction are completely prevented. It ensures continuous, efficient and stable operation of the impurity collection system, so that impurities can be thoroughly and completely collected.
All performance indicators of the equipment strictly comply with GB/T 21158-2025 Complete Set of Seed Processing Equipment national standard. The core parameters are as follows:
Processing productivity: 5–15 t/h (based on wheat);
Seed purity: ≥99%;
Seed selection rate: ≥99%;
Photoelectric sorting purity: ≥99%;
Qualified rate of packaged finished products: ≥99.9%;
Increased breakage rate: ≤0.01%;
Dust concentration in workshop: ≤8 mg/m³;
Equipment operating noise: ≤85 dB(A).
Note: The above indicators are measured on the premise that the original purity of seed raw materials meets national standards.
联系人:熊先生 18168863192
联系人:周先生 13665101927
电 话:0510-83882833
传 真:0510-83882833
地 址:无锡市惠山区玉祁街道芙蓉村蓉丰路
Copyright © 2026 www.wxxbljx.com

手机官网


 苏公网安备32020602001503